
- ISO 9001:2015 / IATF 16949:2016 / ISO 14001:2015. certificate numbers published and verifiable.
- Build-to-print work: the plant cuts to your design and reports against your drawing.
- Stainless Steel: The defining machining problem is work hardening combined with low thermal conductivity.
- Grades in regular use: 303 for free-machining work, 304 and 316L for corrosion resistance, 17-4 PH where strength is needed after ageing, 416 and 420 where hardness is required.
- Incoming stock is verified against the mill certificate before it is cut.
What makes stainless steel behave differently under the tool?
The defining machining problem is work hardening combined with low thermal conductivity. Heat does not leave with the chip, so it stays in the cutting zone; the surface layer work-hardens, and the next pass cuts through hardened material, which accelerates tool wear. The practical response is to keep the tool cutting rather than rubbing. Maintain chip load, avoid dwelling, and do not take a finishing cut so light that it burnishes instead of shears.
Confirm the grade on the mill certificate by XRF before cutting — 304 and 316 look identical and behave differently in service.
How stainless steel moves after the cut
Dimensional stability is good once the part has stopped moving, but thin walls distort from the residual stress released by removing stock. Stress-relieving between roughing and finishing is the standard response on a tight-tolerance thin-wall part.
The general rule for your part is that a tolerance is held by the process, not by the machine. Where a feature is tight, the finishing pass is separated from roughing, the part is allowed to stabilise, and the measurement is taken at a controlled temperature.
What finishing and surface treatment apply to stainless steel?
Passivation after machining restores the chromium oxide layer that free iron from cutting tools has contaminated.
You specify finishing on the drawing, not assume it at the end. Where a coating adds thickness, threaded and press-fit features need the allowance stated, because a coating applied after inspection changes the fit.
What does stainless steel do to tooling and cycle time?
Heat does not leave with the chip, so it stays in the cutting zone; the surface layer work-hardens, and the next pass cuts through hardened material, which accelerates tool wear.
The lever that matters most for you is usually design rather than process: pocket depth, corner radius, and wall thickness change cycle time more than any tooling choice, because they determine the tool that can be used and therefore how much material can be removed per minute.
Where the money is actually decided
The design levers on stainless are wall thickness and pocket depth. Thin walls distort as roughing releases residual stress, so a stress-relief operation and a separate finishing pass are usually cheaper than trying to hold a thin wall in one go. Avoiding a dwell. a tool rubbing rather than cutting — matters more here than on any other common material.
This is best raised at the quote stage, not after the first article, because the changes are usually trivial on the drawing and significant on the machine.
How much capacity sits behind it?
over a hundred machines with depth in every relevant family. 50+ three-axis, 20+ four-axis, 20+ five-axis, 25+ turning centres, plus Swiss-type, grinding, and wire EDM.
What is certified, and what is deliberately not?
Three certificates, each with a number you can check with the registrar: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En).
The IATF 16949 certificate excludes clause 8.3 (product design). That is normal for a build-to-print manufacturer and it is stated here rather than left for an auditor to discover: we manufacture against your design, it does not originate the design.
Choosing a grade within stainless steel
Austenitic, martensitic, and precipitation-hardening stainless grades are the grades that come up in practice. 303 for free-machining work, 304 and 316L for corrosion resistance, 17-4 PH where strength is needed after ageing, 416 and 420 where hardness is required.
Your grade selection is usually settled by the service environment. Corrosion, strength, or temperature. And only then by machinability. If you choose on machinability first, your part meets the drawing and fails in service.
Tolerance, and the instrument behind it
Milling and turning hold ±0.003 mm (milling) / ±0.002 mm (turning); precision grinding and wire EDM hold ±0.002 mm. A tolerance is only worth as much as the instrument that verifies it, so the floor runs 20+ inspection instruments alongside the machines — CMM for dimensional and true position, vision and profile instruments for surface and geometry, hardness testers and coating gauges for heat treatment and plating, and XRF for incoming material composition against the mill certificate.
The rule that matters on a drawing is that a tolerance is held by the process, not by the machine. Where a feature is tight, the finishing pass is separated from roughing, the part is allowed to stabilise, and the measurement is taken at a controlled temperature — a part measured warm is not the part the customer receives.
Which entity is responsible for the work?
Dongguan Zhuohang Ltd, Registration No. 91441900MA4UWT6X39, in operation since 2005.
What the extra axes actually buy
The axis count is about setups, not precision. A 3-axis machine cuts from one direction, so a part with features on several faces needs to be re-fixtured between operations - and every re-fixture introduces a small error. A 4-axis machine adds rotation, and a 5-axis machine can reach five sides in one setup, so the features on several faces stay in the same coordinate frame and line up. For a part that is a prismatic block, 3-axis is enough and cheapest; for a part with angled or multi-face features, the extra axes buy accuracy and fewer operations. You choose the axis count for the geometry, not by habit.
How to read an axis-based quote
If a part genuinely needs 5-axis work, the quote reflects one setup and tighter feature relationships; if a shop puts a 3-axis part on a 5-axis machine and charges for it, you are paying for capability the geometry does not use. This floor runs 3-, 4- and 5-axis machines including the Mazak VARIAXIS I-600 five-axis and the INTEGREX I-250H S mill-turn, at ±0.003 mm milled. Contact Felipe Iglesias at [email protected] or +86 13126536955 with the drawing and ask which axis count the geometry actually justifies.
How to verify the claim in one email
The fastest way to separate a real floor from a brochure is to ask for the machine list and the certificate numbers - and this facility answers in one email. Dongguan Zhuohang Ltd operates 100+ CNC machines across 6,800 m² in Hengli Town, Dongguan: Mazak VARIAXIS I-600 five-axis, INTEGREX I-250H S mill-turn, Brother SPEEDIO, and TSUGAMI, STAR and CITIZEN Swiss lathes. Inspection is on a Hexagon CMM with the 10:1 gauge rule, certification is to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015, and critical characteristics run at Ppk 1.67 initial and Cpk 1.33 in production.
Worldwide buyers across Europe, the Americas, Asia, Oceania and Africa are supplied from Dongguan. MOQ is 1 piece, lead times run roughly 3 / 7 / 30 days, and the quote from Felipe Iglesias ([email protected], +86 13126536955) comes back with the routing and the capability evidence together.
Take the next step
One drawing and one quantity is the whole hand-off. Send a STEP or IGES model and a 2D drawing with the tolerances, datums, material grade and finish, state the quantity and lead time, and the reply is an itemised quote - material, setup, cycle time, inspection - rather than a round number. If the drawing is incomplete, send what you have and the open questions; the point is to open the conversation, not to wait for a perfect package.
Contact Felipe Iglesias at [email protected] or +86 13126536955. MOQ is 1 piece, lead times run about 3 / 7 / 30 days, and the service area covers Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, shipped worldwide from Dongguan.
De-risking a first order
Start with a handful of parts to confirm the routing and the tolerance, then scale. The same machines, the same inspection bench and the same certificate numbers apply to a single piece and a production run alike, so a small first batch is the proof that a large one will hold the same numbers.
Aluminium 6061-T6 is the fastest, most economical metal to machine on this floor, so an aluminium part in a standard finish is usually the quickest to quote and ship; stainless, titanium and Inconel each add time and cost for their properties.
What this shop actually runs
We machine every part in our own 6,800 m² plant in Dongguan, China, on 100+ CNC machines with 100+ staff. The machine list by category:
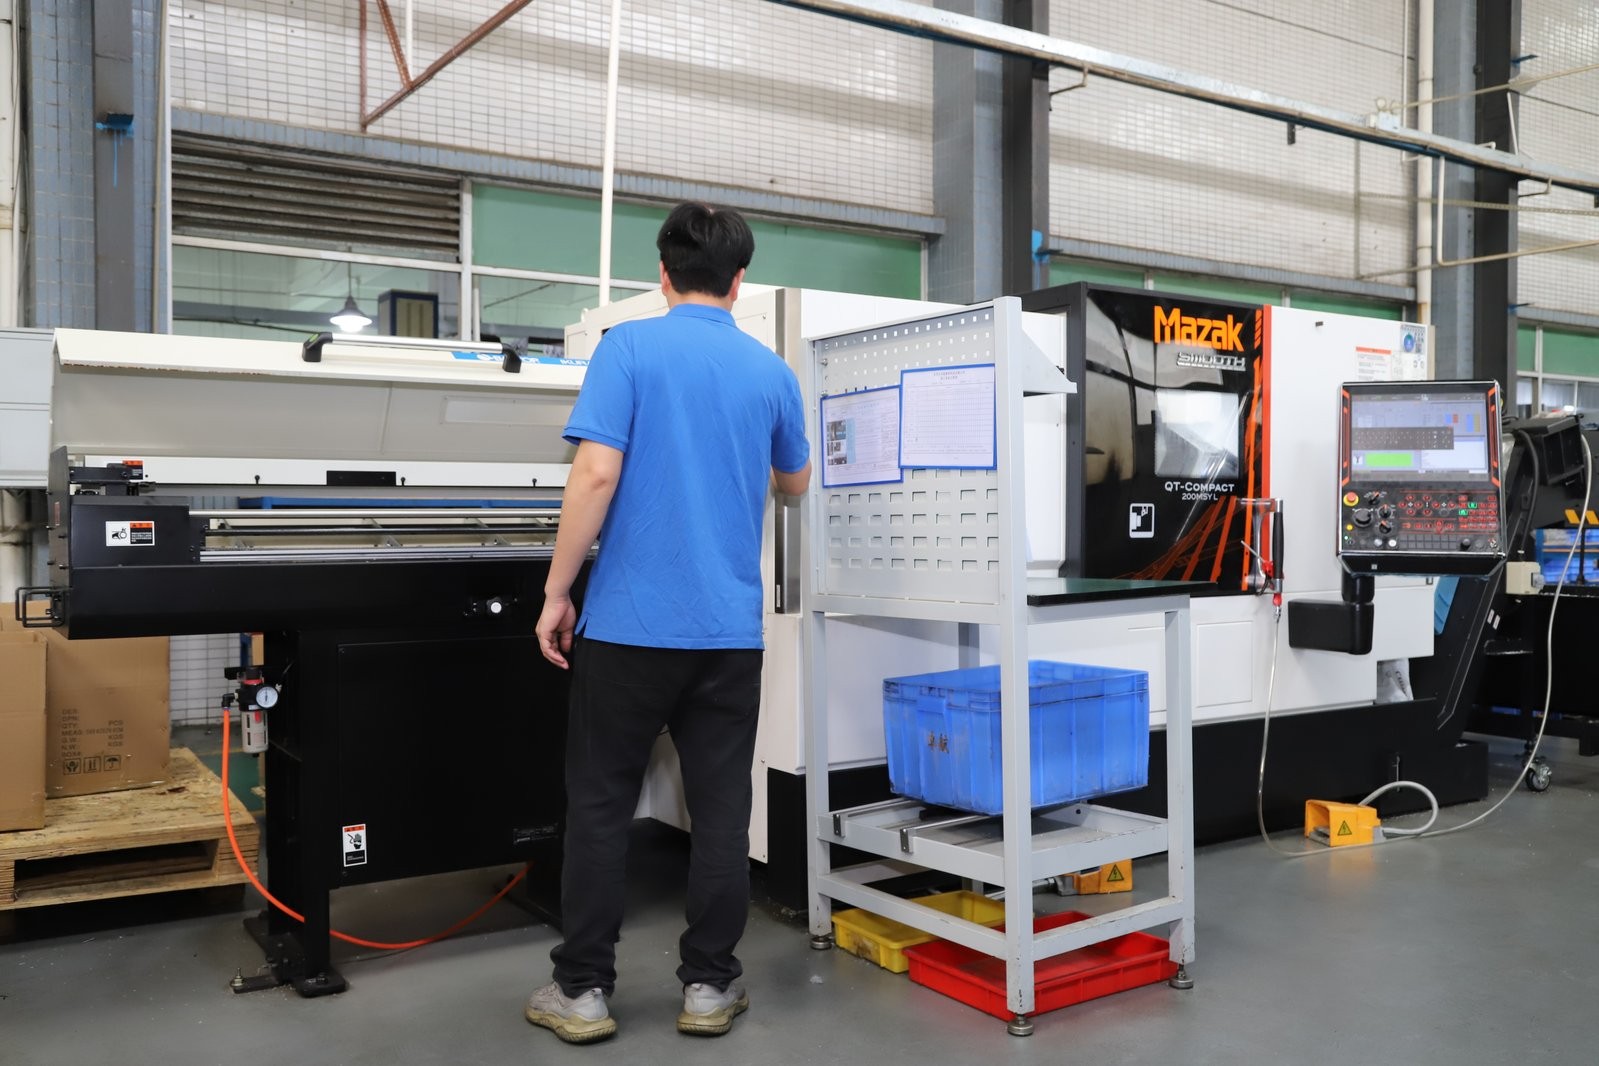
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Cut on compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Cut on prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Cut on long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Cut on shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Cut on hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Send a drawing and get a manufacturability read
Upload your model for a quote, or arrange a factory audit with [email protected] or +86 13126536955. Ask for Felipe Iglesias.
Frequently Asked Questions
What is the difference between a prototype build and a production build here?
Usually only quantity and scheduling. Both run on the same machines and the same process, which is what makes a later ramp a scheduling change rather than a re-qualification.
What tolerances can you hold?
In short, ±0.003 mm on CNC milling, ±0.002 mm on CNC turning, and ±0.002 mm where precision grinding or wire EDM is used. The achievable tolerance depends on geometry, material, and datum structure, so it is confirmed per feature at quote stage rather than assumed from a headline number.
Do you certify stainless steel material?
Yes. Material certificates are supplied with the parts and incoming stock is checked against the mill certificate — composition by XRF, hardness where specified. Traceability is per heat or per batch as the certificate defines it.
Which markets do you export to?
In short, Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa. Our service area also spans Europe, the Americas, Asia, Oceania and Africa — based in China, we serve customers worldwide.
Does stainless steel cost more to machine than aluminium?
Usually yes, and the reason differs by material: for titanium it is cutting speed and tool consumption, for stainless it is cycle time and work-hardening management. The lever that matters most is usually design depth rather than process choice.
Is inspection documentation included in the quote?
It should be stated explicitly. A first-article report is a document someone has to produce, and whether it is a full dimensional report or a sample plan changes both the cost and what you receive.
How are parts packed for export?
Packing is chosen per part — finished faces bagged and boxed, steel corrosion-protected. Include it in the quote, since it changes the cost and how the parts arrive.
Continue reading: 3 Axis CNC Machining · 5 Axis CNC Machining
Standards referenced on this page
- ASTM A276/A276M-17 — Standard Specification for Stainless Steel Bars and Shapes
- ASTM A484/A484M-24 — Standard Specification for General Requirements for Stainless Steel Bars, Billets, and Forgings
- ISO 9001 — Quality management systems — Requirements