
Aluminum or stainless steel is the most common material question a machining buyer faces, and on a 4-axis part the answer matters more than usual because the part has earned its place on a rotary axis through multi-face geometry, thin walls, or features that must hold position across faces. Those are exactly the situations where the material's stiffness, thermal behavior, and machinability decide whether the part works. This guide compares the two families grade by grade, with the machining angle a 4-axis buyer actually needs and a decision table you can bring to the next design review.
Why does the material call matter more on a 4-axis part?
On a simple 3-axis bracket, a material mistake costs a re-run. On a 4-axis part, the same mistake is expensive twice. First, the programming, fixturing, and inspection that surround a multi-face part are identical for both materials — switch alloys after quoting and you redo the quote, the schedule, and possibly the tooling. Second, the geometry that justifies a rotary axis — thin walls, deep pockets, features on multiple faces — is exactly where material stiffness and deflection show up.
The machining-side difference matters too. Aluminum cuts at high speed with light forces, so thin-wall aluminum features can be pushed hard even as the rotary axis indexes. Stainless is roughly three times stiffer than aluminum but cuts at a fraction of the speed, work-hardens if the tool dwells, and conducts heat poorly. On 4-axis work there is a compensating advantage: holding a complex stainless part in one rigid, indexed setup reduces the deflection and re-clamping stress that cause problems in work-hardening alloys. Both families are entirely machinable on a 4-axis machine when the program respects their behavior.
What do 6061-T6 and 7075-T6 give you in aluminum?
6061-T6 is the workhorse. Its yield strength of about 276 MPa is modest, but it machines cleanly at high speed, holds ±0.003 mm milling tolerances without drama, and takes anodize reliably, which makes it the default for housings, brackets, and prototypes across industries. Its density of 2.70 g/cm³ is about a third of steel, and its thermal conductivity is roughly ten times that of stainless, which is why heat-management parts are almost always 6061.
7075-T6 is the upgrade when the design is strength-limited. Its yield strength of about 500 MPa approaches some steels at a third of the weight, which is why it appears in structural and aerospace-adjacent parts. The costs of that strength: roughly two to three times the stock price of 6061, slightly slower machining, and lower corrosion resistance in some conditions, so 7075 parts are usually anodized or painted in service. On thin-wall 7075 parts, residual stress can move the geometry after machining, which is exactly the kind of problem a rigid single-setup 4-axis process controls well.
Confirm the temper is available in the bar size you need before the drawing is finalized. 7075-T6 is stocked in common rounds and plates, but odd sections may need longer lead times, and the drawing should allow the tempers the market actually carries. A grade that is hard to source as certified bar costs you in both price and schedule, so let the factory confirm availability at quoting rather than discovering it mid-order.
Which stainless grades matter for machined parts?
Stainless is a family, not a material, and the grades differ in both the part and the quote. All sit near 7.9 g/cm³ — about three times denser than aluminum — with a Young's modulus near 193 GPa, giving roughly three times the stiffness of aluminum for the same geometry.
| Grade | What it is | Machining behavior | Typical 4-axis parts |
|---|---|---|---|
| 303 | Free-machining austenitic; added sulfur breaks chips | Best machinability of the family; bright finish | Fittings, valve stems, sensor housings, fasteners |
| 304 | General-purpose austenitic | Moderate; work-hardens if cuts are light or tools dwell | Structural and food-contact parts, enclosures |
| 316L | Adds molybdenum for chloride and pitting resistance; low carbon | Moderate; tougher on tooling than 304 | Marine, chemical, and pharmaceutical components |
| 17-4PH | Precipitation-hardening martensitic | Machines well annealed; strong after heat treatment | High-strength structural parts, actuators |
The rule of thumb: 303 when you need a corrosion-resistant machined part at the lowest machined cost, 304 when the part is also welded or formed, 316L when chlorides and process chemicals are in the picture, and 17-4PH when you need real strength rather than corrosion resistance alone.
When is 17-4PH the right stainless over 304 or 316L?
If the part is a housing that keeps water out, 304 or 316L is fine. If the part carries load — a clevis, a link, a bracket in a mechanism that sees vibration — the annealed austenitics cap out near 200–300 MPa yield, and a strong stainless part becomes a big, heavy part. 17-4PH solves that: in the H900 condition it reaches yield strengths around 1100 MPa, stronger than most carbon steels, while keeping the corrosion resistance of the family.
That strength changes the design conversation. A load-bearing stainless part in 17-4PH can be smaller and lighter than the equivalent 304 design, which is why aerospace actuators, valve components, and precision mechanisms specify it. The trade-offs are scheduling: 17-4PH is machined soft, heat-treated, and then finished, so the tolerance strategy must account for a treatment step and a finishing pass between roughing and final size. A shop that manages that sequence will hold the tight geometry; one that treats heat treatment as an afterthought will not.
Strength, stiffness, and weight: when does aluminum win?
Run the numbers on the load case rather than the brochure. If weight is the constraint — the part rides on a robot arm, a vehicle, or an aircraft — aluminum wins outright: 7075-T6 delivers a strength-to-weight ratio that most steels cannot match. If the constraint is stiffness in a fixed envelope — the part must not deflect and you cannot make it bigger — stainless wins, because its modulus advantage overcomes its weight.
Then add the thermal facts. Aluminum conducts heat roughly ten times better than stainless, so heat sinks and thermal paths stay in aluminum. Aluminum's higher thermal expansion means a precision assembly that cycles through wide temperature swings needs the differentials designed out — a stainless shaft in an aluminum housing is a classic pairing for exactly that reason, with the fit calculated at the working temperature rather than at 20 °C. For thin-wall accuracy during machining, aluminum's low cutting forces let the machine hold fine features without deflection, while a stainless thin wall demands slower, shallower cuts, which a rigid 4-axis setup accommodates by keeping the tool engaged and the vibration low.
Corrosion and environment: when do you have to move to stainless?
Aluminum protects itself with a native oxide film that is excellent in dry, indoor air, so machined housings sit happily in electronics for decades. The film fails where chlorides and moisture concentrate: coastal salt air, road salt, chemical washdowns, and process fluids. In those environments bare aluminum pits, and anodize only postpones it, because the coating is thin and any scratch or cut edge re-exposes the substrate.
That is the line that forces a move to stainless. Salt water and marine spray point to 316L; food processing with repeated caustic washes points to 304 or 316L with passivation; industrial chemicals call for a grade matched to the media. Passivation — removing free iron from the surface and restoring the chromium oxide layer — is what makes machined stainless live up to its name. If the environment is aggressive, design in stainless from the start rather than hoping a coating will save an aluminum part.
Watch for galvanic coupling when the design mixes the families. Where stainless fasteners or fittings contact aluminum in a damp environment, the aluminum becomes the anode of a galvanic cell and corrodes faster than it would alone; isolating washers, anodize on the aluminum, or a deliberate choice of compatible hardware are the standard answers. The material decision is therefore not always one metal for the whole assembly — it is often aluminum structure with stainless hardware, managed properly rather than avoided entirely.
How do finish and tolerance strategy differ between the families?
Both families reach the same machined tolerances, but their finishing routes differ completely. Aluminum's standard finish is anodize — clear or dyed, with hard anodize (Type III) for wear — and the coating is part of the surface the drawing specifies. Stainless takes no anodic coating; its treatments are passivation for corrosion and electropolishing for a clean, smooth finish, and sealing or seating surfaces are ground to ±0.002 mm rather than coated.
The tolerance strategy differs in the details, not the numbers. Aluminum's thermal expansion means a precision part machined in a warm shop can measure differently in a cold inspection room — measurement temperature matters, and both the factory and your incoming inspection should measure at the standard temperature. Stainless work-hardens, so the machining strategy keeps the tool engaged with consistent chip load; on a 4-axis machine that means the program avoids letting the tool dwell between indexed faces. Neither behavior limits the achievable tolerance — production capability stays at ±0.003 mm CNC milling, ±0.002 mm CNC turning, ±0.002 mm grinding, with Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window, but both demand the machining and measurement discipline matched to the alloy.
Name the surface finish on the drawing as well as the material. As-machined aluminum typically lands at a fine Ra without extra cost, while a specified fine finish on stainless may add a pass or a polishing step; stating the value you need — rather than "good finish" — lets the factory quote the actual work instead of guessing at your intent.
What changes on the quote when you switch alloys?
Switching from aluminum to stainless changes three lines at once. Material: stainless stock runs roughly two to four times the cost of 6061-T6 per kilogram, with 316L and 17-4PH above the middle of that band. Machining: stainless cuts at a fraction of the speed of aluminum, so the same geometry consumes more spindle minutes — commonly two to four times on comparable features. Finishing: anodize on aluminum versus passivation or electropolish on stainless are different vendor steps with different costs.
The calendar moves too. Stainless grades in common sizes are usually stocked, but 17-4PH adds a heat-treatment leg between roughing and finishing, and certified lots add the incoming verification step. A design change from aluminum to stainless after quoting is effectively a new project: new material line, new machining strategy, new finish, new date. The decision table below is the summary to keep on the wall.
Availability shapes the quote as well. Aluminum tempers in common rounds and plates are stocked everywhere; some stainless grades and heat-treated tempers are available only to order, which adds both cost and days. Ask the factory which grade it stocks and let the drawing reference the standard tempers the market actually carries. A grade that is hard to source as certified bar costs you twice — in price and in schedule.
| Decision driver | Choose aluminum | Choose stainless |
|---|---|---|
| Weight is the constraint | 6061-T6 or 7075-T6 | Only if strength demands steel |
| Stiffness in a fixed envelope | Thicken the section | 304 or 316L — modulus wins |
| Strength under load | 7075-T6 | 17-4PH |
| Salt, chemical, or washdown duty | Only with robust coating | 316L plus passivation |
| Heat dissipation | 6061-T6 | Poor conductor; avoid |
| Thin-wall accuracy in one setup | Light cutting forces | Rigid setup controls work hardening |
| Lowest machined cost at low volume | 6061-T6 | Rarely |
| Wear and surface hardness | Hard anodize | As-machined or hardened 17-4PH |
For the full cost picture behind the switch — where the machining-time multiplier lands and how the fixed lines spread across quantity — the 4-axis CNC machining cost guide works through the numbers. When the duty is clear and the grade is on the drawing, the quote and the part both behave.
What this shop actually runs
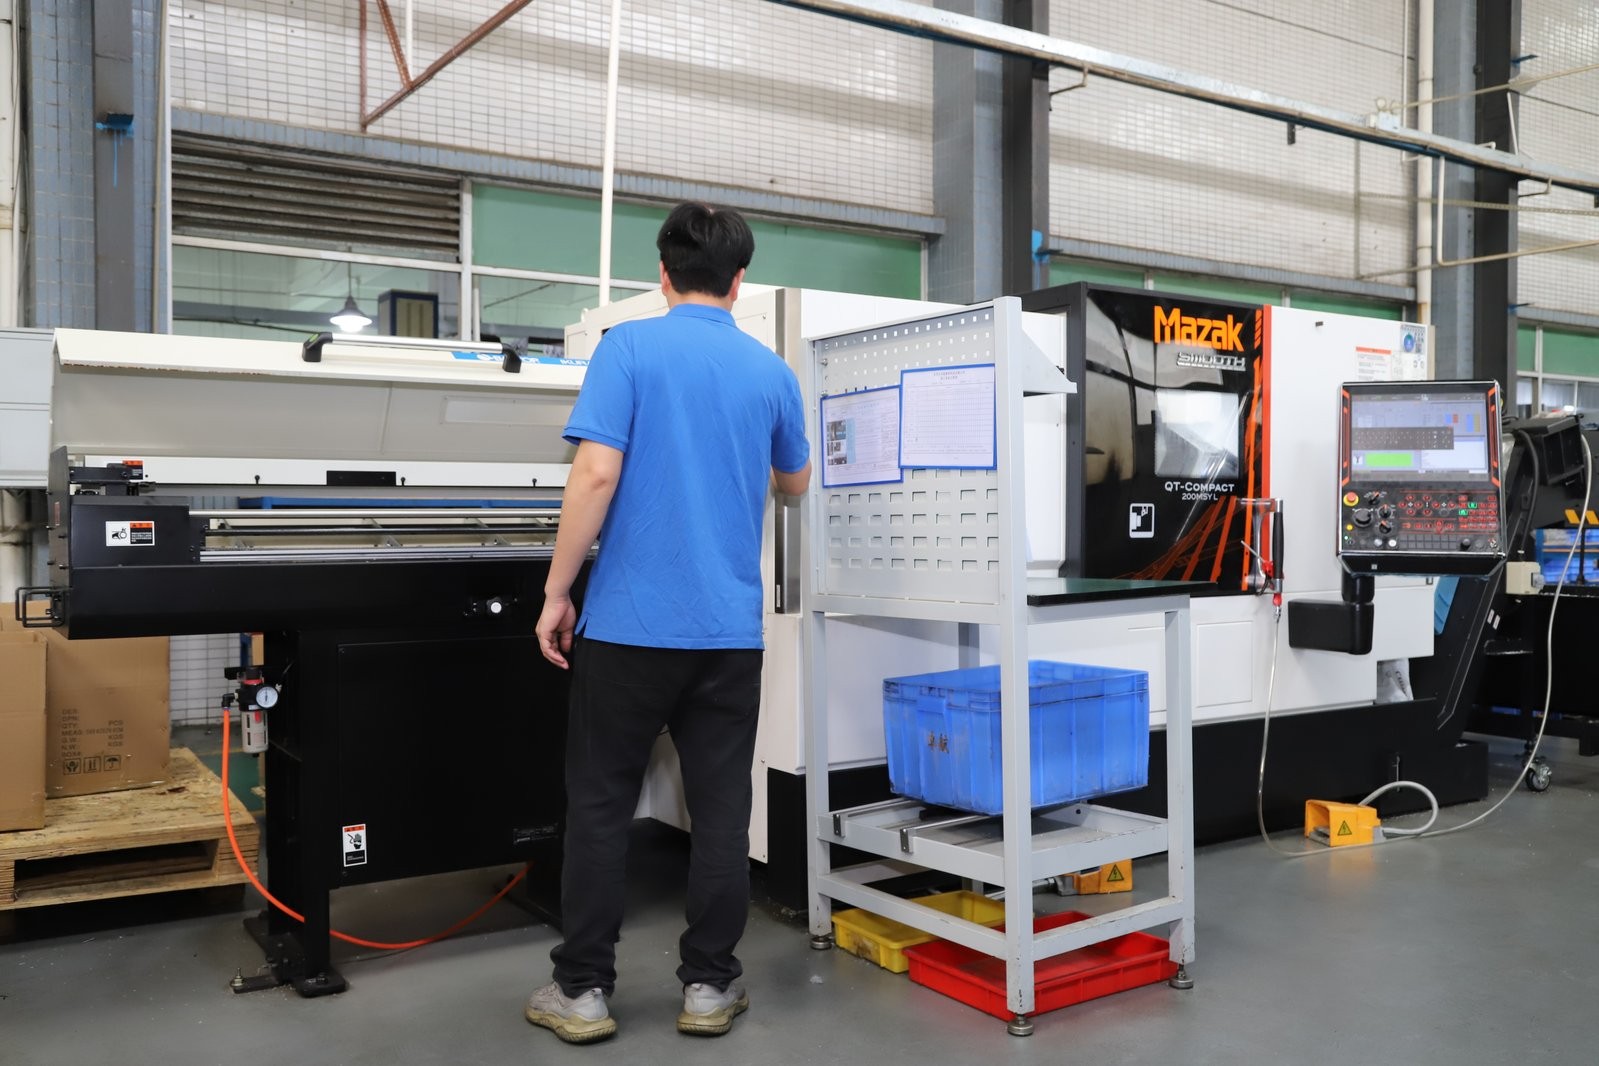
We machine every part in our own 6,800 m² plant in Dongguan, China, on 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Cut on compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Cut on prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Cut on long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Cut on shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Cut on hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Not sure which alloy fits the duty?
Send the STEP or IGES model and the service conditions to [email protected] or call +86 13126536955. You will get a material recommendation with the machined-cost difference shown, not just a quote for the grade you guessed.
Frequently Asked Questions
Is 6061-T6 or 7075-T6 better for a 4-axis machined part?
In short, 6061-T6 is the everyday choice: it machines easily, holds tolerance, anodizes well, and is the cheapest aluminum to cut. Choose 7075-T6 when the design is strength-limited and weight matters, because its yield strength is roughly 80 percent higher than 6061-T6, and accept the higher stock cost and lower corrosion margin in some environments.
Which stainless grade is easiest to machine?
In short, 303 is the free-machining grade: its sulfur content breaks chips and keeps cutting forces low. 304 and 316L are tougher and more prone to work hardening, and 17-4PH machines acceptably annealed and is heat-treated afterward.
When should I choose stainless over aluminum?
In short, When the part needs corrosion resistance without coatings, stiffness in a small envelope, higher-temperature capability, or wear resistance. Aluminum wins on weight and thermal conductivity, so choose aluminum when those matter more and the environment is mild enough for anodize to protect the part.
Does 4-axis machining change how stainless machines?
In short, It helps in a specific way: holding a complex stainless part in one indexed setup with a rigid fixture reduces deflection and re-clamping stress, which are the enemies of accuracy in work-hardening alloys. It does not change chip behavior or cutting speeds — stainless still cuts at a fraction of the speed of aluminum.
Will anodized aluminum protect a part as well as stainless?
In short, For indoor and mild outdoor duty, hard anodize gives aluminum useful wear and corrosion resistance. It is not a substitute for stainless where chlorides, chemicals, or process fluids are present, because the coating is thin and a scratch re-exposes the aluminum.
How much more does a stainless version cost?
In short, Stainless stock runs roughly two to four times the cost of 6061-T6 per kilogram, and the cutting is slower, so machining time rises on top. As a working guide, converting a simple aluminum part to 304 can multiply the machined-part cost by two to four; complex geometry in 17-4PH or 316L can move more.
What tolerance can each material hold on a 4-axis machine?
In short, Both hold the same production capability — ±0.003 mm (milling) / ±0.002 mm (turning) on milled and turned features and ±0.002 mm by precision grinding, with Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window.
What material documentation should I ask for?
In short, Ask for mill certificates and confirmation that incoming material was verified against the certificate before cutting. Incoming lots are XRF-checked against the mill certificate at this shop, so the alloy on the drawing is the alloy that reaches the machine.
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM A276/A276M-17 — Standard Specification for Stainless Steel Bars and Shapes
- ISO 9001 — Quality management systems — Requirements