
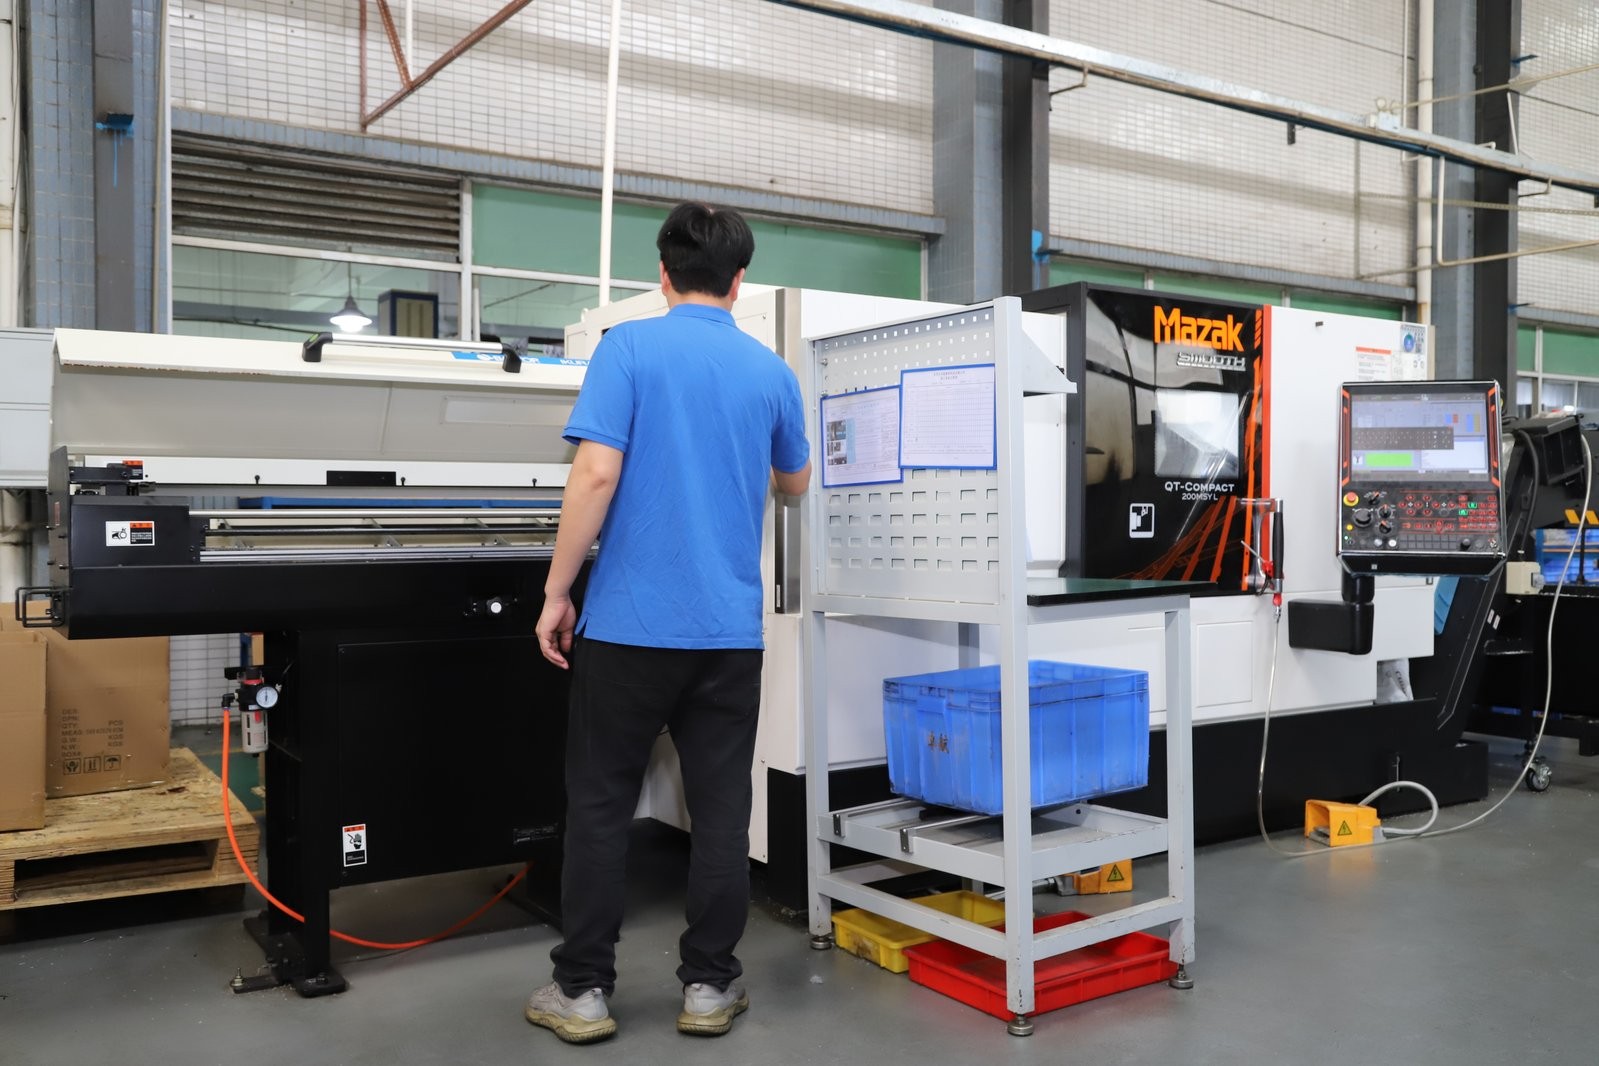
What Torque Turning Services Cover
Turning removes material as the part spins; "torque" emphasizes the machine's ability to push hard on large or tough stock without chatter. Multi-axis turning adds live tooling (milling flats, slots, cross-holes while the part is chucked) and a sub-spindle (working the back face without re-fixturing). For rotational parts — shafts, bushings, couplings, fittings — this is almost always the cheapest, most accurate route, because concentricity is held naturally in a single clamping.
How It Works in Practice
The bar or blank is gripped, the main spindle turns the front features, live tools cut any off-axis geometry, then the part transfers to the sub-spindle for the back side. A bar feeder keeps high-volume work running unattended. The buyer benefit: every diameter and cross-feature is cut in one setup, so runout and face-to-face relationships stay tight without manual handling.
Materials and Process Options
Torque turning handles aluminum, stainless, titanium, brass, copper, and steel — including the harder grades where spindle torque matters. It is the first choice for axisymmetric parts and a strong companion to milling: a near-round part with a few milled features finishes complete on a multi-axis lathe, avoiding a second trip to a mill. For non-round geometry, milling wins; route accordingly.
Specifying Torque Turning: Tolerances, Finishes, RFQ Checklist
The tolerances to watch are concentricity and position of off-axis features, not just diameters. Send:
- Model + drawing with diameters, concentricity, and cross-hole position called out.
- Material grade and certification.
- Surface finish on sealing diameters (Ra) if the part mates with a bearing or seal.
- Volume and whether bar feed or chucked blanks suit the geometry.
Common Mistakes Buyers Make
The usual error: sending a round part to a mill-only shop and paying a premium for what a lathe does in a third of the time. The second: ignoring runout on long thin shafts — specify steady-rest support when the length-to-diameter ratio is high. The third: not confirming the shop's live tooling can reach your off-axis feature, forcing a surprise second setup.
How Zhuohang Precision Machining Factory Approaches Turning
Turning and milling are integrated here, so a part goes to whichever process is cheapest for its geometry. Our multi-axis lathes with live tooling and sub-spindles finish many rotational parts complete in one cycle, then we verify critical diameters and positions on CMM. Same quality system as our broader CNC machining services — ISO 9001:2015 and IATF 16949:2016, with Cpk reporting on production.
How to verify the claim in one email
The fastest way to separate a real floor from a brochure is to ask for the machine list and the certificate numbers - and this facility answers in one email. Dongguan Zhuohang Ltd operates 100+ CNC machines across 6,800 m² in Hengli Town, Dongguan: Mazak VARIAXIS I-600 five-axis, INTEGREX I-250H S mill-turn, Brother SPEEDIO, and TSUGAMI, STAR and CITIZEN Swiss lathes. Inspection is on a Hexagon CMM with the 10:1 gauge rule, certification is to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015, and critical characteristics run at Ppk 1.67 initial and Cpk 1.33 in production.
Worldwide buyers across Europe, the Americas, Asia, Oceania and Africa are supplied from Dongguan. MOQ is 1 piece, lead times run roughly 3 / 7 / 30 days, and the quote from Felipe Iglesias ([email protected], +86 13126536955) comes back with the routing and the capability evidence together.
Take the next step
One drawing and one quantity is the whole hand-off. Send a STEP or IGES model and a 2D drawing with the tolerances, datums, material grade and finish, state the quantity and lead time, and the reply is an itemised quote - material, setup, cycle time, inspection - rather than a round number. If the drawing is incomplete, send what you have and the open questions; the point is to open the conversation, not to wait for a perfect package.
Contact Felipe Iglesias at [email protected] or +86 13126536955. MOQ is 1 piece, lead times run about 3 / 7 / 30 days, and the service area covers Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, shipped worldwide from Dongguan.
Tolerance and surface finish reference
±0.003 mm milled, ±0.002 mm turned, and ±0.002 mm ground or wire-cut, all verified on a Hexagon CMM against the datum scheme. Surface finishes span Ra 0.8 to 3.2 µm as-milled, Ra 0.2 to 0.4 µm ground, and Ra 0.05 to 0.1 µm polished. The 10:1 gauge rule governs every feature - the instrument must resolve ten times finer than the tolerance it checks. And the datum is what makes the tolerance real: read against two different datums, the same callout gives two different parts, so state the datum and the convention, ASME Y14.5 or ISO.
Placing the part on the right process
The shortest way to a correct part is to let the shop read the drawing and place it on the right machine, because the process follows the geometry, the material and the tolerance - not the label on the page. A part with a turned profile goes to the lathe, a prismatic part to the machining centre, a long thin part to a Swiss machine, and a sheet or panel to the router; you state what the part must do, and the shop matches the process. That is the whole of the routing decision, and it is settled at the quote.
This floor runs 100+ CNC machines - Mazak VARIAXIS I-600 five-axis, Mazak INTEGREX I-250H S mill-turn, Brother SPEEDIO, and TSUGAMI, STAR and CITIZEN Swiss lathes - at ±0.003 mm milled and ±0.002 mm turned, verified on a Hexagon CMM, with certification to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015. MOQ is 1 piece and lead times run roughly 3 / 7 / 30 days. Send the drawing to Felipe Iglesias at [email protected] or +86 13126536955 and the process is matched to the part.
The quality evidence behind every part
Every part ships with its evidence. Incoming stock is checked against the mill certificate - composition by XRF, hardness where specified - before machining. The first article is inspected in full against the drawing, critical characteristics run under statistical process control at Ppk 1.67 initial and Cpk 1.33 in production, and in-process checks hold the tolerance on a Hexagon CMM with the 10:1 gauge rule. The final report ships with the parts, so you get the product and the proof in one delivery - the line between a held tolerance and a claimed one.
your guide to quoting
Behind every good quote is a drawing that specifies. Name the material grade, not just the material; mark the datums and tolerances that actually matter; state the finish; and give a quantity, even a range. The more the drawing specifies, the less the shop assumes, and the closer the quote is to the real part. An itemised quote - material, setup, cycle time, inspection - lets you challenge the right line rather than negotiate blind, and it is the quickest path to a cheaper part: loosen a tolerance that does not matter, or raise the quantity to spread the setup. Send the drawing to Felipe Iglesias at [email protected] or +86 13126536955 and ask for it itemised.
What the torque number actually governs
Torque is not a finish you can call out in the abstract - it is the product of the diameter, the run-out, the balance, and the fit of the shaft against its mating bore. A part that must transmit torque without wobble needs a turned diameter with low run-out, a balanced assembly, and a clean shoulder for the bearing to seat against. If you specify the torque and the speed, plus the run-out and balance the application tolerates, you get a part that runs true; if you only write "torque turning", you leave the shop to guess at what the part is actually for.
This floor turns the shaft, the housing and the rotor on 100+ machines, checks run-out and concentricity on a Hexagon CMM, and holds Ppk 1.67 or better initial and Cpk 1.33 or better in production on the critical diameters. State the torque, the speed and the balance requirement, and the quote reflects the real service.
Balance and vibration
A rotating part that transmits torque also vibrates, and the vibration is a balance and run-out problem, not a tolerance problem. The shop turns the part true and checks the run-out, then balances the assembly where the speed demands it. State the operating speed and the acceptable vibration on the drawing, and the quote includes the balance step rather than discovering it after the part is running.
\nThe result is a rotating assembly that holds its tolerance and its balance through the run, not just on the first article.
\nSend the drawing and the speed requirement, and the routing follows the part.
\nDe-risking a first order
Start with a handful of parts to confirm the routing and the tolerance, then scale. The same machines, the same inspection bench and the same certificate numbers apply to a single piece and a production run alike, so a small first batch is the proof that a large one will hold the same numbers.
Aluminium 6061-T6 is the fastest, most economical metal to machine on this floor, so an aluminium part in a standard finish is usually the quickest to quote and ship; stainless, titanium and Inconel each add time and cost for their properties.
Send the model and the volume, and the quote returns with the routing, the tolerance and the certificate attached.
What this shop actually runs
We machine every part in our own 6,800 m² plant in Dongguan, China, on 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Cut on compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Cut on prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Cut on long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Cut on shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Cut on hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Have a rotational part? Send the drawing to [email protected] or use our RFQ checklist for a turning-vs-milling recommendation and a transparent quote.
Frequently Asked Questions
When is turning cheaper than milling?
For any axisymmetric part — shafts, bushings, fittings — turning is faster and holds concentricity naturally. Multi-axis turning adds milled features in the same cycle, avoiding a second setup at a mill.
What tolerances can torque turning hold?
In short, Diameters to ±0.003 mm (milling) / ±0.002 mm (turning) standard; concentricity and position are governed by single-chucking accuracy. For the tightest relationships, finish-turning or grinding follows.
Do I need a sub-spindle?
Only if the part has features on the back face. A sub-spindle lets the machine finish both ends in one cycle; without it, the part is re-chucked manually, adding a setup, time, and a small accuracy risk.
Continue reading: 1/4" Acrylic CNC Cutting
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM B348/B348M-21 — Standard Specification for Titanium and Titanium Alloy Bars and Billets
- ISO 9001 — Quality management systems — Requirements